Spiral Conveyor
2 MB
Spiral Conveyor – Single Lane
MONK Conveyors build spiral conveyor systems using Apollo VTS’s world’s leading vertical conveying systems. Apollo VTS based in The Netherlands manufacture leading high-quality machines.
The Apollo Single Lane Spiral Conveyor transports products up or down in a continuous flow and has proven to be a very reliable spiral conveyor system that increases efficiency while conserving valuable floor space.
Lorem ipsum
Trusted by
MONK is a UK-based conveyor and automation specialist with over 25 years’ experience in conveyor systems, conveyor manufacturing, system integration and industrial automation.
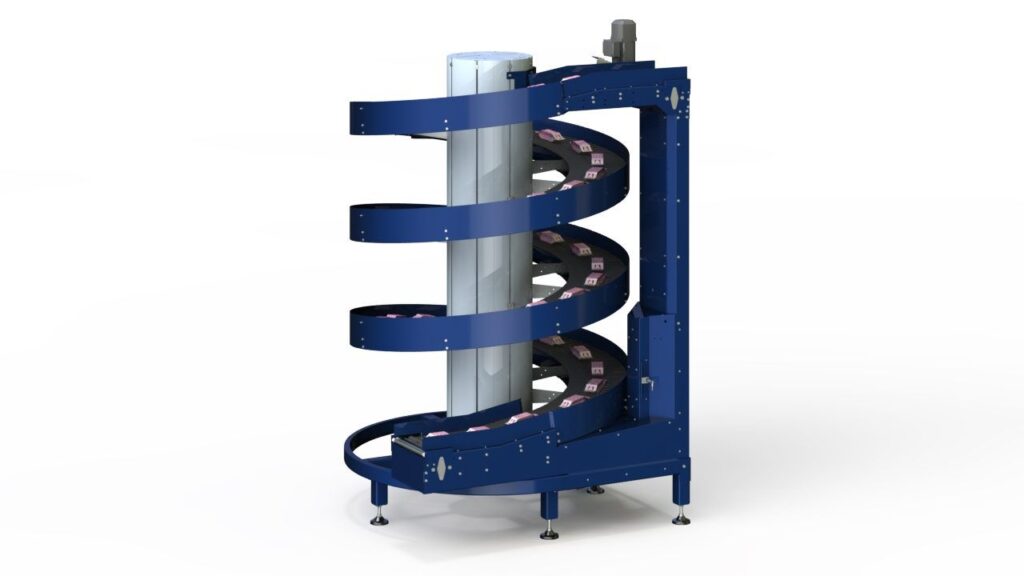
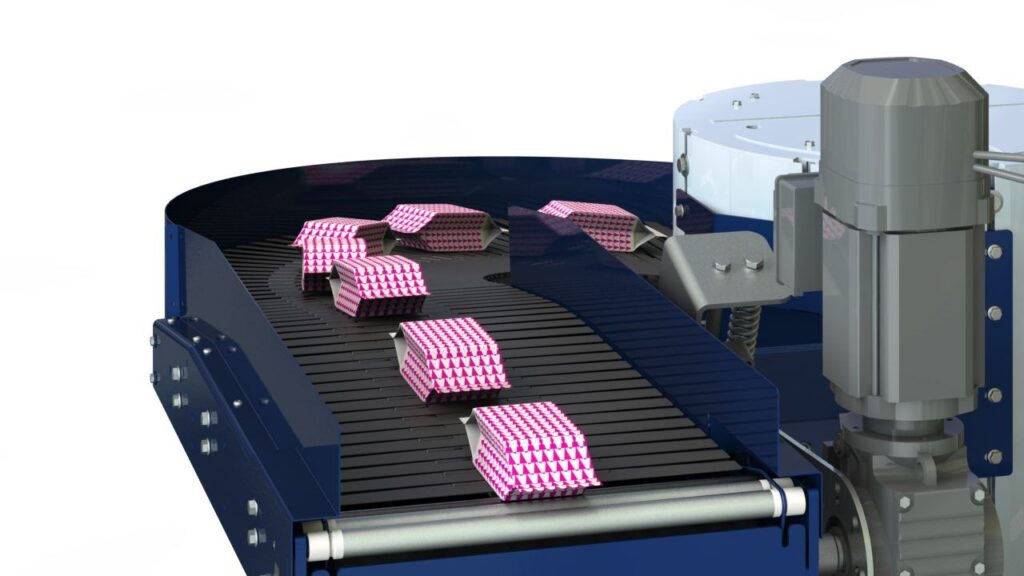
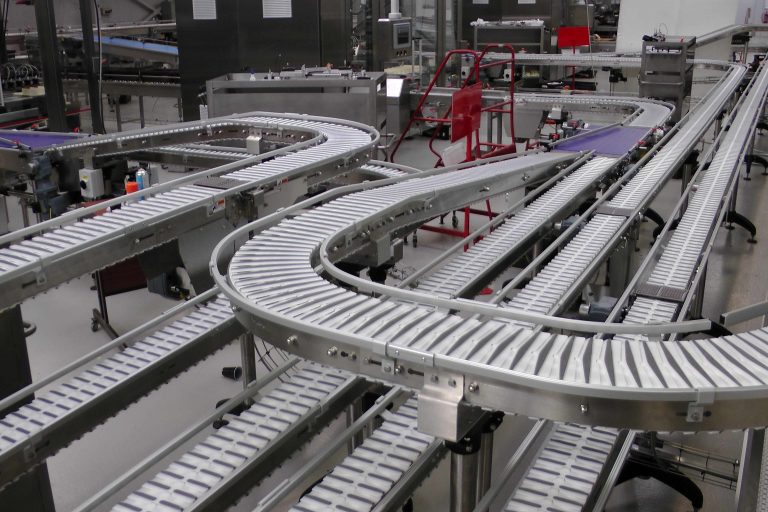
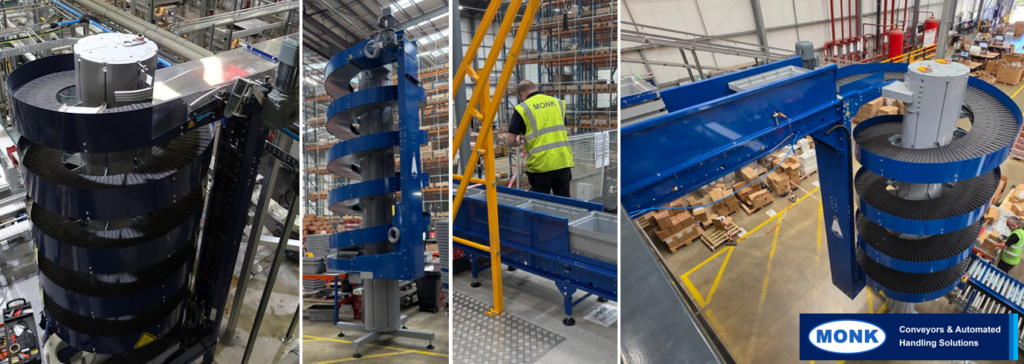
The Spiral Conveyor consists of a moving belt which revolves around a central column. It can be used to move a wide range of products between floor levels or over walkways. The spiral belt guide system runs on precision bearings so there is only rolling friction and therefore the noise level is very low.
Multiple products are suitable for a spiral conveyors such as; bags, bundles, totes, trays, cans, bottles, containers, cartons and wrapped and unwrapped items. Spiral systems work for many types of industries: food industry, beverage industry, newspaper industry, pet food & personal care industry and others.
Dual Lane Spiral Conveyors and Mass Flow Spirals are also available. Please contact us for further information at Monk Conveyors.
Loads up to 50 kg/meter
Speed 60 m/minute
One motor
Designed to operate 24/7
Small footprint
Low friction operation
Built-in protection
Low noise level
No lubrication under the slats needed
Low maintenance
The Dual Lane Spiral Conveyor from Apollo transports materials and products up or down in a continuous flow. Similar to the Single Lane Spiral Conveyor, but the Dual Lane Spiral Conveyor transports double the capacity, which results in twice as much throughput. This makes our Dual Lane Vertical Conveying System an efficient and reliable option for businesses with higher capacity needs, but a limited amount of floor space for handling systems.
Loads up to 50 kg/meter
Speed 60 m/minute
Two separately driven tracks
Operate 24/7
Small footprint
Low friction operation
Built-in protection
Double capacity
Low noise level
No lubrication under the slats needed
Low maintenance
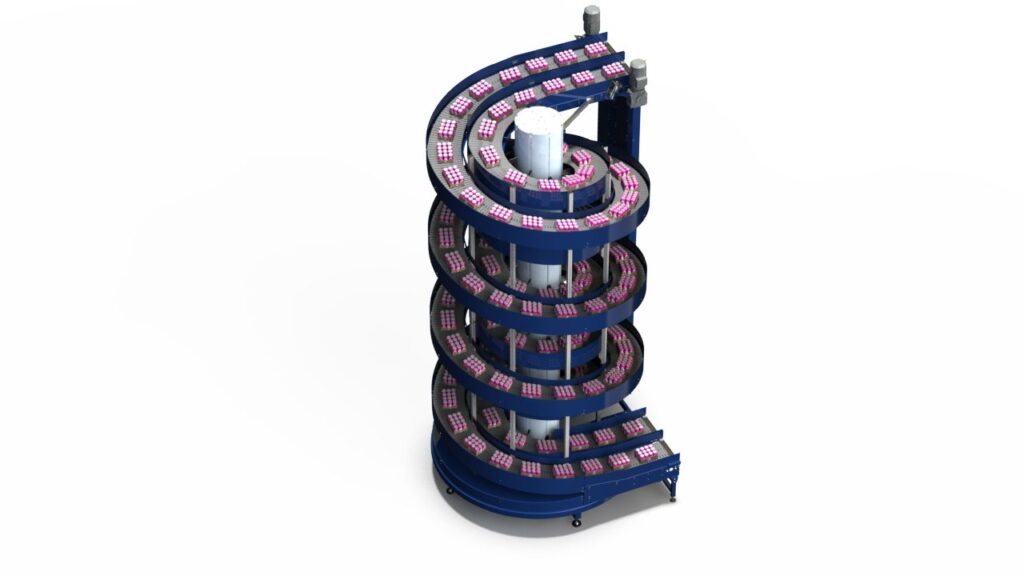
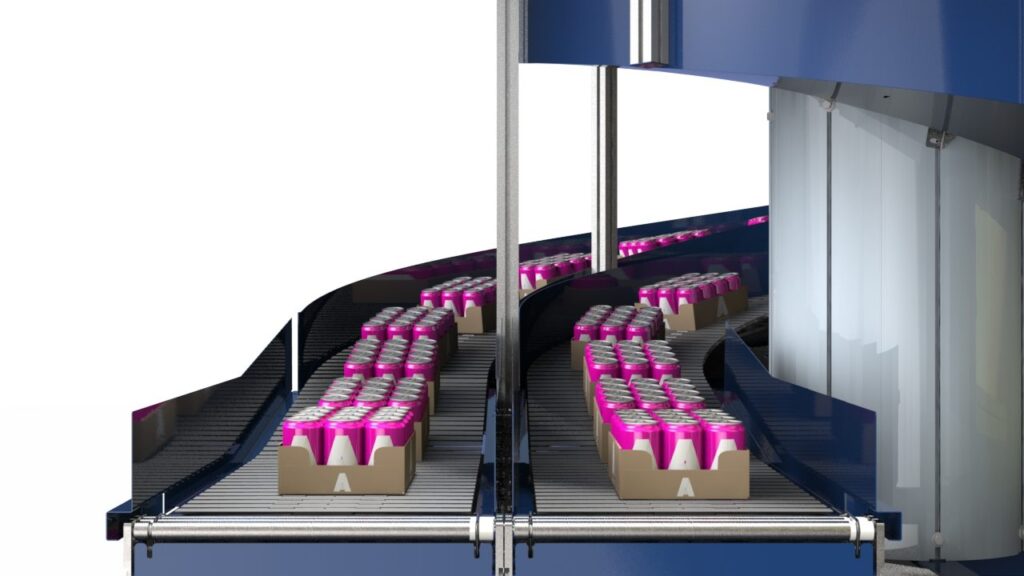
This Vertical Spiral consists of two separately driven conveyor belts that revolve around a centre. It can be used to move a wide range of products between floor levels or over walkways. The spiral belt guide system runs on precision bearings so there is only rolling friction and noise level is very low.
There are multiple products which are suitable such as; bags, bundles, totes, trays, cans, bottles, containers, cartons and wrapped and unwrapped items. Spiral Conveyor systems work for many types of industries: food industry, beverage industry, newspaper industry, pet food & personal care industry and others.
The Apollo Dual Lane Spiral Conveyor has two tracks that are separately driven. The two tracks can be synchronized with the same speed, run at different speeds, or run in the opposite directions with the same or different speed.
The two tracks of the Dual Lane Spiral Conveyor can be delivered in different widths, and it is also possible to have the two lanes with different infeed and outfeed heights.
Single Lane Spiral Conveyors and Mass Flow Spirals are also available. Please contact us for further information at Monk Conveyors.