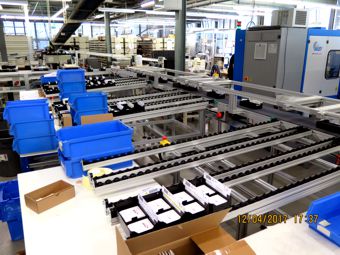
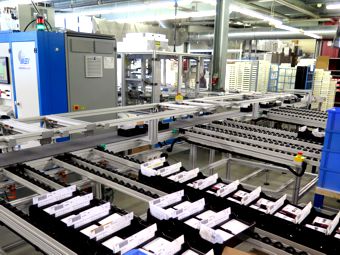
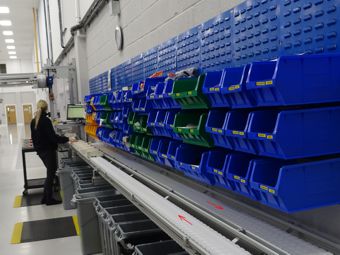
Optical Lab Packing Conveyor
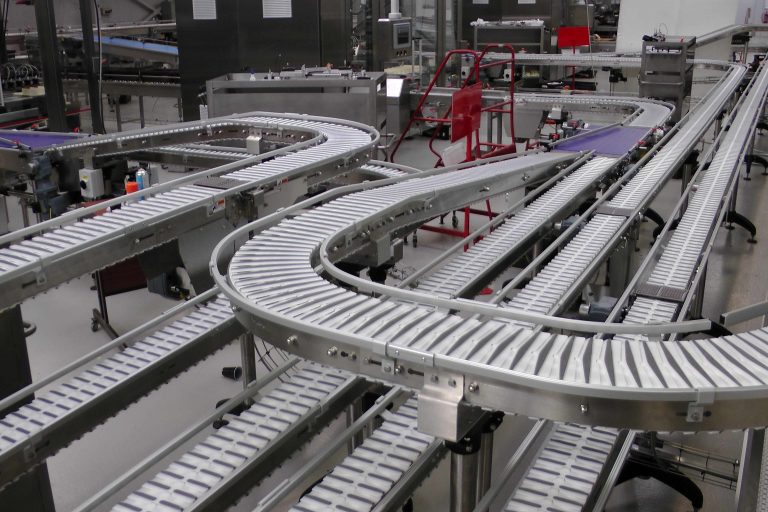
Optical lab packing conveyors are suitable for feeding from the end of a number of production lines and cells. Work is merged together to feed to the dispatch area. Lifters or incline conveyors can be used to feed over walkways. Empty job trays can then be feed back to the start of the system.
Trusted by
Fitting Big Efficiency into Small spaces
MONK is a UK-based conveyor and automation specialist with over 25 years’ experience in conveyor systems, conveyor manufacturing, system integration and industrial automation.
Key Features
Sensors, bar-code readers and control a control system manage the flow of trays
Line mimic with fault flags for rapid fault finding
Track can pass over machines and walkways
Lifters are used to take the trays to high level and bring them down to floor level again
A continual flow of work can be maintained
HMI touch screen is used for easy operation
High level track can be used to save floor space
Ceiling or floor supports
Emergency stop safety circuit